
A pipeline coating inspection is only useful later if someone can connect the result to the right piece of pipe, the coating system and the conditions under which it was applied. A folder of unsigned reports or photographs named by date can leave an operator with plenty of information and very little usable evidence.
A good coating handover package makes that connection clear. It should let the receiving team find a location, understand the acceptance requirements, review what was measured and see how defects were resolved. Agree on the package before coating starts, while the contractor can still capture the information efficiently.
Define the scope and the acceptance basis
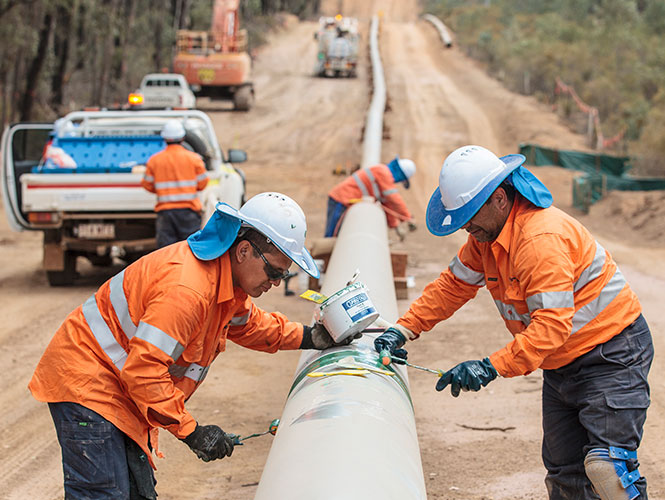
Start with the work covered: factory coating, field joints, rehabilitation or individual repairs. Identify the approved coating system, project specification, inspection and test plan, application procedure and document revisions. List the responsible contractor, inspector and person authorized to release the work.
Standards have specific scopes. For example, ISO 21809-3:2016 addresses qualification, application and testing of field-joint corrosion coatings. Its published scope excludes additional mechanical protection, thermal insulation and concrete weight-coating joint infill. If those layers are included in the project, make their acceptance evidence identifiable too. Avoid treating one coating certificate as approval of the complete joint assembly.
Use the contractually applicable editions and approved procedures. A public summary of a standard cannot supply every acceptance limit or replace the controlled documents used on the job.
Give each coated location a traceable identity
Choose identifiers that remain meaningful after installation. Depending on the project, these could include pipe numbers, weld numbers, stationing, an agreed coordinate reference and repair numbers. Connect them to the as-built register rather than creating an unrelated numbering system for coating inspection.
For each location, link the coating product and relevant component batch numbers to the application date and crew record. Where the approved procedure requires evidence of storage conditions, shelf life or mixing, retain it with the same reference. Photographs help when their captions identify the location, orientation, date and feature being shown.
As a practical check, ask someone unfamiliar with the work to locate one photographed repair using the register. If they need the original inspector to explain it, improve the identification before handover.
Preserve the preparation and application evidence
The finished surface cannot tell the receiving team everything about the steel underneath. Keep the preparation inspection and application records required by the project, including the specified cleanliness assessments, surface-profile measurements and contamination checks where applicable.
Environmental readings should be associated with a time and work area. A temperature or humidity entry from the start of a shift may not explain conditions when another joint was coated hours later. Record application and curing information at the intervals required by the approved procedure, with any interruptions or departures documented.
This is a records checklist, not a universal preparation specification. The product, substrate, exposure and approved procedure determine which measurements and limits apply.
Make test results interpretable
A report that says “passed” should also show what was tested, how it was tested and which acceptance criteria were used. Preserve the measured results and their locations, including units. Keep instrument identification and the calibration or verification evidence required by the applicable method.
For holiday detection, DeFelsko’s ASTM G62 guidance describes reporting the specimen identity, instrument, verification method and test method. It also identifies voltage information for high-voltage testing. These details let a reviewer understand a result instead of relying on an unexplained check mark.
Record the voltage actually used and its approved basis. DeFelsko explains that insufficient voltage can miss defects, while excessive voltage can damage the coating. Selection belongs with the applicable standard, coating requirements and qualified inspection procedure. Do not insert a generic volts-per-thickness rule into the handover form.
Connect each defect to its repair and reinspection
Give every reported defect a reference that follows it through disposition, repair and acceptance. Record its location, the approved repair method, material used, repair date and subsequent inspection results. Retain the original finding alongside the closeout so the repair history remains understandable.
For U.S. pipelines subject to the relevant Part 195 requirements, 49 CFR 195.561 requires inspection of the specified external coating immediately before lowering into the ditch or submerging, and repair of discovered damage. Build the project workflow around that timing. An earlier inspection does not document damage that might occur during later handling.
Finish with an index and a clear release status
Organize the final package so a reviewer can move from the asset register to the applicable reports without guessing. A useful index groups:
- Approved specifications, procedures and revisions
- Location and material traceability records
- Preparation, application and inspection reports
- Defect, repair and reinspection records
- Approved deviations, outstanding items and release signatures
Keep unresolved items visible and distinguish a conditional release from final acceptance. Agree on the archive owner and retention schedule. 49 CFR 195.589 includes corrosion-control record requirements with different retention periods, so one blanket deletion date may be inappropriate.
The final test is simple: can the next person explain what was installed, where it was inspected and why it was accepted? A handover package that answers those questions is useful both at construction closeout and when the pipeline needs attention later.