
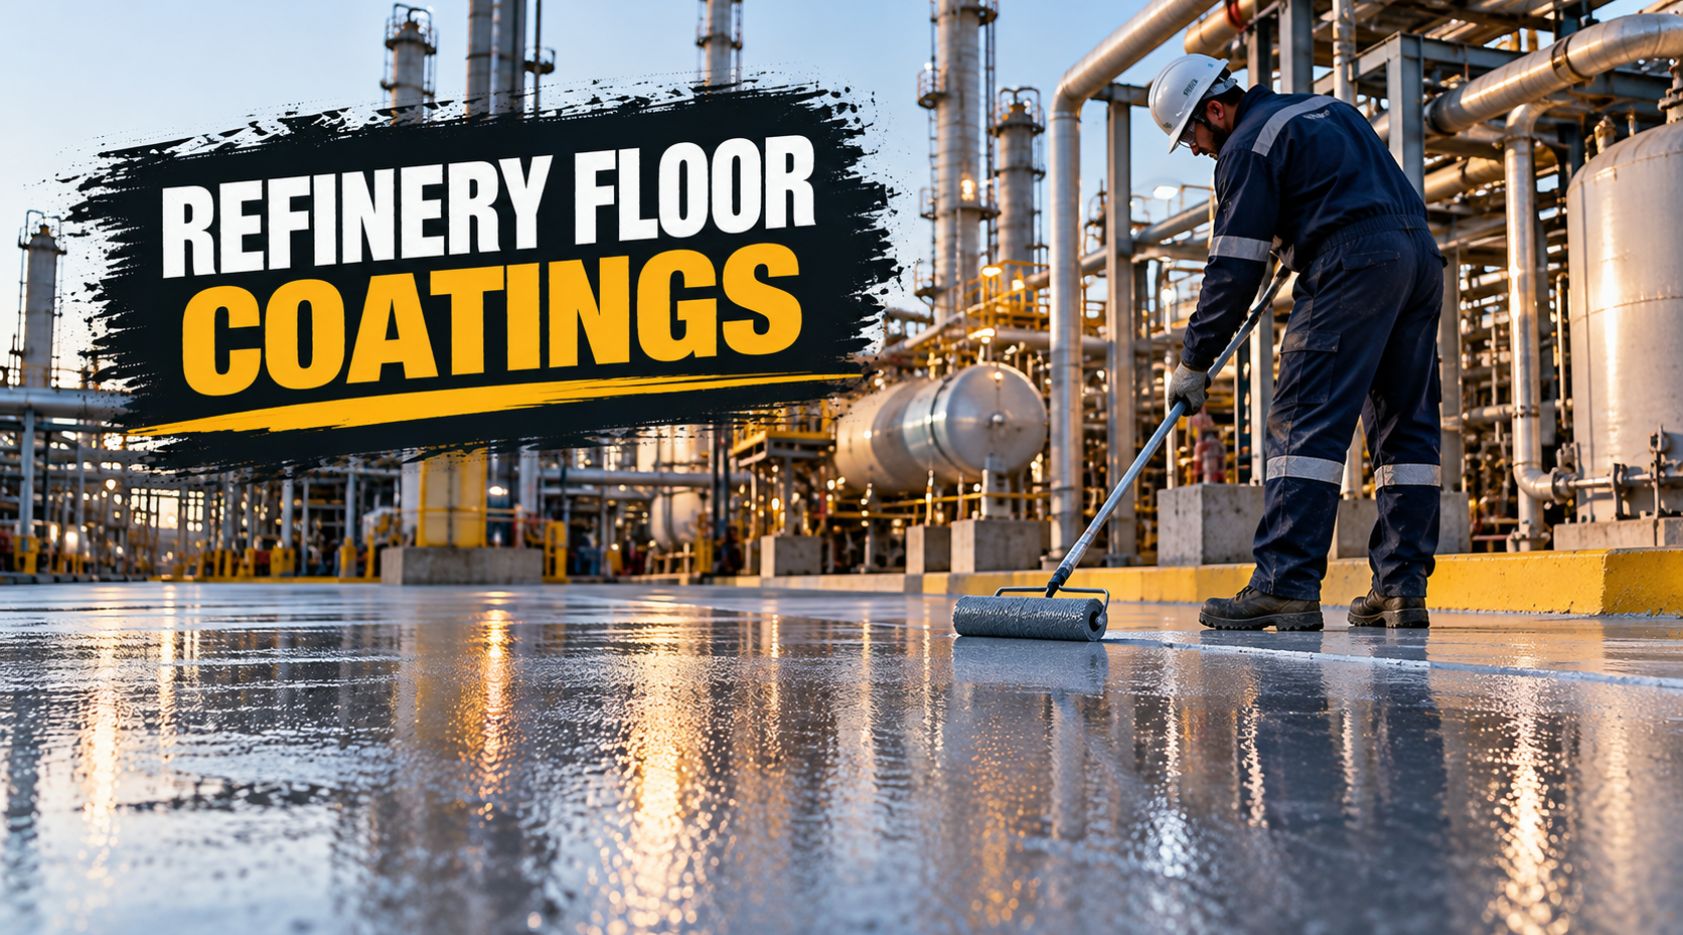
Walk a refinery process unit after a rough week and the floors tell the story. Dark staining under a pump seal. A pale bloom where something acidic dripped. A hairline crack along a joint that wasn’t there at the last turnaround. Refinery floor coating chemical resistance is usually the first question anyone asks when a pad needs protection, and it’s a fair one. But the floors that fail early tend to fail for a second reason too: heat. A hot fluid landing on cold concrete, or a steam hose passing over a coated pad, does damage that no chemical resistance chart ever mentions. This guide covers both problems, how they interact, and how to match a floor system to what your process area actually sees.
What a Refinery Process Floor Actually Goes Through
Most industrial floors deal with one or two kinds of abuse. A refinery process floor gets nearly all of them. Hydrocarbons of every weight drip from pump seals, sample points, and flanges. Solvents, caustic from treating operations, and acids in certain units all find their way onto concrete sooner or later, along with amines, process water carrying chlorides, and whatever cleaning chemicals the crews use afterward. On top of the chemistry, there’s heat from hot oil leaks and steam cleaning, daily temperature swings, vacuum trucks, maintenance vehicles, dropped tools, and scaffolding dragged across the surface.
Bare concrete handles almost none of this well. It’s porous, so hydrocarbons wick deep into the slab. Acids attack the cement paste and leave a dusty, weakened surface. Once concrete is saturated with oil, it’s slippery, hard to clean, and a housekeeping headache that never really goes away. A good floor system gives you a dense, cleanable barrier that keeps spills on the surface where they can be removed instead of soaking in where they can’t.
Refinery Floor Coating Chemical Resistance: What the Ratings Actually Tell You
Here’s where a lot of specifications go wrong. A chemical resistance chart lists chemicals, but the rating attached to each one depends on conditions that are easy to overlook: concentration, temperature, and how long the coating stays in contact.
Most ratings describe splash and spill exposure with reasonably prompt cleanup, which is a very different situation from continuous immersion. A pump pad that sees occasional drips is a completely different problem from a sump or trench holding process liquid for days. A coating that handles one comfortably can fail quickly in the other, even though the chemical on the chart is identical.
Concentration matters just as much. A dilute acid and a concentrated one can behave nothing alike against the same coating, and higher temperatures speed up chemical attack, sometimes dramatically. Mixtures complicate things further. A blend of solvents can be harder on a coating than any one component alone.
So the practical advice is simple. Don’t accept “chemical resistant” as an answer. Ask the manufacturer for documented resistance data covering the exact chemicals, concentrations, and temperatures your area sees, and be clear about whether the exposure is occasional splash or sustained contact. For critical areas, a test patch or immersion testing on the actual system is cheap compared with relining a unit.
Thermal Shock: The Failure Nobody Sees Coming
A coating and the concrete underneath it expand and contract at different rates. When temperatures change slowly, that mismatch is manageable. When they change fast, it isn’t. A steam hose passing over a pad, a hot process fluid spilling onto cold concrete, or a hard rain hitting a sun-baked slab can all create sudden temperature swings, and the stress concentrates right at the bond line between coating and substrate.
That stress shows up in a few ways. Thin, rigid films can crack. Coatings with a thermal expansion rate far from concrete’s can debond in sheets. And heating a slab from above can drive moisture vapor toward the bond line, producing blisters even when the coating itself is chemically fine.
Different systems handle this differently. Thicker cementitious urethane systems are generally chosen for areas with hot washdown or hot spills, in part because their thermal behavior sits closer to concrete’s. Flexible systems with high elongation tolerate movement by stretching rather than cracking. Rigid epoxies perform well chemically but can be the most vulnerable when temperature swings are severe. There are standard tests that probe this, such as ASTM C884, which evaluates thermal compatibility between concrete and an epoxy resin overlay, but a test number is only a starting point. Ask for thermal cycling or thermal shock data on the specific system, at the temperatures your area really experiences, and check the maximum service temperature on the data sheet rather than assuming.
Comparing Common Floor System Options
| System | Chemical Resistance Profile | Thermal Shock Tolerance | Cure and Downtime | Typical Role |
|---|---|---|---|---|
| Epoxy novolac | Broad, generally stronger than standard epoxy | Limited in thin rigid films | Moderate, hours to days depending on system | General chemical process areas |
| Vinyl ester | Very strong against many acids and solvents | Varies, depends on build and formulation | Moderate, more demanding application | Severe chemical exposure |
| Urethane cement | Good, formulation dependent | Generally strong, designed for hot washdown | Moderate, thicker build | Areas with heat and washdown |
| Polyurea or hybrid polyurea | Varies, can be limited against some strong acids and solvents | Flexible, tolerates movement well | Fast, short return to service | Containment, crack bridging, tight schedules |
| Polyaspartic | Varies by formulation | Varies | Fast | Topcoat or thin-build systems |
Read that table as a starting point, not a verdict. Every row says “varies” somewhere for a reason. Two products in the same category can perform very differently, and the data sheet and resistance data for the actual product should always outrank a general comparison like this one.
It’s also worth being honest about one thing: no system wins everywhere. Fast-cure polyurea systems are attractive when downtime is the main constraint, but they aren’t automatically the right answer for a trench holding strong chemicals. Epoxy novolac and vinyl ester earn their place in severe chemical service, but they’re less forgiving of movement and heat. Matching the system to the dominant threat, rather than defaulting to whatever is most familiar, is most of the job.
Surface Preparation in Oil-Soaked Concrete
Preparation is where refinery floors get tricky. Concrete that has absorbed hydrocarbons for years holds that contamination well below the surface, and coatings don’t bond reliably to oil-saturated substrate no matter how good the product is. Depending on how deep contamination runs, preparation can mean aggressive mechanical removal of the contaminated layer, followed by profiling and repair, rather than a routine blast and coat.
Moisture testing matters here too, especially on slab-on-grade pads where vapor can push up from below, and so does adhesion testing on a trial area before committing to a full pad. The principles are the same ones covered in our guide to preparing a surface before coating application, which is written around pipelines but applies directly: remove contamination, achieve the profile the manufacturer requires, and verify instead of assuming. When floor coatings fail early, the post-mortem almost always points back to preparation, a pattern our root cause analysis of coating failures explores in more detail.
Planning Around Turnarounds and Operating Units
Most refinery floor work happens in tight windows. Planned turnarounds compress everything into a fixed schedule, and in operating units, work often has to proceed in sections around live equipment, under permits and facility safety procedures. Those procedures, along with the product’s safety data sheet, govern how and when coating work can proceed. They aren’t something to improvise around.
Cure speed becomes a real selection factor in that environment. A system that returns to service in hours instead of days can mean the difference between finishing inside the window and carrying work into the next one. Fast-cure chemistries, like the polyaspartic systems discussed in our look at rehabilitation coatings where speed and durability both matter, show how much schedule flexibility that can buy. Speed has trade-offs, though. A faster cure leaves less working time, and a system that cures quickly but doesn’t match the chemical exposure is a bad trade no matter how good the schedule looks.
Details That Decide Whether a Floor Lasts
Coatings rarely fail in the middle of a field of flat floor. They fail at details: curb bases, trench edges, drain rims, expansion joints, and transitions between different surfaces. These are the places where movement concentrates and where a thin or poorly terminated coating gives out first. Good specifications spell out how the coating terminates at curbs and drains, how joints are treated, and what sealant goes into moving joints. That sealant needs to be compatible with the same chemicals as the coating itself, or the joint becomes the weak link.
Slip resistance deserves equal attention. A smooth coating is easy to clean but treacherous when wet or oily, while a heavily textured one grips well but traps contamination. Most process areas land somewhere in between, using aggregate broadcast sized for the exposure. General workplace rules, including OSHA’s walking-working surface requirements, expect floors to be kept free of slipping hazards, so this isn’t just a comfort issue.
Process areas are often also subject to secondary containment requirements, which vary by facility, product handled, and jurisdiction. Which rules apply, and what they require of the floor and its curbing, should be confirmed for the specific site rather than assumed.
Coverage and Specification Notes
For sprayed or rolled coatings, coverage follows the standard math: one gallon at one mil covers 1,604 square feet. Thicker troweled or broadcast systems are specified by thickness and mix design instead, so quantities should always come from the manufacturer’s technical data sheet for the exact system and thickness specified, not from a general rule applied across product types.
Inspection and Maintenance
A refinery floor coating isn’t something you install and forget. Regular walkdowns catch the early signs: discoloration near spill points, softening or blistering, cracking along joints, and damage at curb bases and drain edges. Small damage deserves fast repair, because chemicals migrate under a compromised coating and spread the problem well beyond the visible spot.
Cleaning practices matter too. Aggressive solvents or the wrong detergent can slowly damage a coating that was perfectly capable of handling the process chemicals it was specified for. Keeping a simple inspection record, with dates, locations, and repair notes, makes it far easier to see whether a recurring problem is tied to a specific exposure and to plan recoats before a failure forces one.
Frequently Asked Questions
What coating is best for refinery process area floors?
There isn’t a single best choice. The right system depends on the chemicals involved, the temperatures and thermal shock the area sees, and how much downtime is available. Epoxy novolac, vinyl ester, urethane cement, and polyurea systems each have areas where they make the most sense.
How can I tell if a floor coating will resist a specific chemical?
Ask for documented resistance data at the exact chemical, concentration, temperature, and exposure type involved. For critical areas, test patches or immersion testing on the actual system give much more confidence than a general rating.
What is thermal shock, and why does it crack floor coatings?
Thermal shock is a rapid temperature change, such as a hot spill or steam cleaning on a cold slab. Because the coating and concrete expand at different rates, sudden changes create stress at the bond line that can crack or debond the coating.
Can a refinery floor be coated while a unit is operating?
Sometimes, in sections and under the facility’s permits and safety procedures. Whether it’s feasible depends entirely on the site’s rules and the specific area, and the product’s safety data sheet and site procedures should govern the work.
Does oil-soaked concrete need to be removed before coating?
Often, at least the heavily contaminated layer. Coatings don’t bond reliably to oil-saturated concrete, so contamination depth needs to be assessed and the surface prepared accordingly, with adhesion testing before the full application.
How often should refinery floor coatings be inspected?
Routine visual walkdowns should be frequent, with more formal periodic inspections scheduled according to exposure severity and the facility’s own program. High-exposure areas like trenches, sumps, and curb bases deserve more attention than open, lightly used floor.
Conclusion
Refinery floor coating chemical resistance is only half of the picture. A system can handle every chemical on the list and still fail because of thermal shock, poor preparation, or a detail at a curb or joint nobody thought about. The floors that last are the ones where the system was matched to the dominant exposure, the data behind that match was documented rather than assumed, the surface was prepared for the contamination actually present, and the details were treated as seriously as the field. Get those four things right and the floor does its job quietly. Get one wrong and the process area will let you know.